





Why Choosing an ISO 9001 Certified Cable Manufacturer Matters?


ISO 9001 Manufacturer: Why Choosing an ISO 9001 Certified Cable Manufacturer Ensures Long-Term Electrical Safety
When you walk through a newly wired commercial building, an industrial plant, or even your own home, you rarely look behind the drywall. You trust that the miles of hidden copper and shielding carrying invisible high-voltage power will just work. We flip switches, plug in machinery, and power up critical infrastructure under the quiet assumption that the wire inside the wall won’t degrade, overheat, or spark a catastrophic failure.
That blind trust is heavily misplaced if the electrical cables behind your walls were manufactured in an environment without rigorous quality governance. In electrical engineering and industrial procurement, reliability isn’t an accident—it is a tightly controlled, repeatable manufacturing science.
If you are sourcing wiring for a major infrastructure project, an industrial facility, or even high-load solar DC arrays, specifying an ISO 9001 certified cable manufacturer is the single most effective safeguard against long-term electrical hazards.
What is ISO 9001 Certification in Cable Manufacturing?
To understand why certification matters, we first need to strip away the corporate jargon and look at what ISO 9001 actually represents on a factory floor.
Published by the International Organization for Standardization, ISO 9001 is the global benchmark for a Quality Management System (QMS). It doesn’t tell a factory what to make; instead, it dictates how they must make it. For a cable manufacturing plant—where a microscopic variance in copper purity, conductor gauge thickness, or PVC insulation extrusion can lead to catastrophic electrical resistance down the road—ISO 9001 acts as an unyielding operational blueprint.
A certified facility must prove consistency across every single phase of production:
- Raw Material Sourcing: Verifying that electrolytic-grade copper (minimum 99.9% purity) and high-grade PVC, XLPE, or LSZH insulation polymers come from verified, traceable vendors.
- Process Control: Maintaining precise temperature profiles during wire drawing, annealing, and polymer extrusion to prevent micro-fissures or brittle spots in the conductor.
- Traceability: Ensuring that every batch of cable can be traced back from the final distribution spool all the way to the specific raw material lot and extrusion machine operator.
Without this level of systemic oversight, a cable factory is essentially operating on guesswork. With it, every meter of cable rolling off the production line adheres to strict, verifiable quality tolerances.
The Hidden Dangers of Uncertified Cable Manufacturing
Electrical failures rarely happen on day one. A sub-standard cable might pass a quick continuity test right after installation. The real danger reveals itself years down the line under thermal stress, mechanical vibration, and peak load conditions.
When procurement teams buy cheap, uncertified wire to shave initial project costs, they often inherit invisible, high-stakes engineering flaws:
1. Sub-Gauge Conductors and High Electrical Resistance
Copper is expensive. Unscrupulous, uncertified manufacturers sometimes shave microscopic fractions off the conductor diameter or use recycled scrap copper laden with impurities. According to Ohm’s law and the Joule heating effect ($P = I^2R$), increased electrical resistance ($R$) leads directly to excessive heat generation ($P$) under load. Over time, this chronic overheating degrades insulation, accelerates aging, and drastically increases the risk of thermal runaway and electrical fires.
2. Inferior Insulation and Dielectric Breakdown
Insulation isn’t just plastic wrapping; it is a critical dielectric barrier rated to withstand specific voltage thresholds. Uncertified facilities often cut corners on plasticizer formulations or use inconsistent extrusion pressures. This results in thin spots, air voids, or moisture-trapping micro-fractures in the insulation. Over months of thermal expansion and contraction, these weak points break down, leading to micro-arcs, short circuits, and complete system failure.
3. Lack of Environmental and Flame-Retardant Resilience
Modern industrial and commercial applications demand specialized sheathing—whether it is Low Smoke Zero Halogen (LSZH) for confined indoor spaces or UV-resistant cross-linked polyethylene (XLPE) for outdoor solar DC installations. Uncertified manufacturers often skip expensive chemical stabilizing agents. As a result, their cables crack under sunlight, emit toxic black smoke during a thermal event, or degrade rapidly when exposed to oils and moisture.
How ISO 9001 Directly Translates to Electrical Safety
When a cable manufacturer operates under a certified Quality Management System, safety is built into the workflow through systematic risk mitigation. Here is how ISO 9001 directly protects your infrastructure:
Stringent In-House Testing and Metrology
ISO 9001 mandates strict calibration and maintenance schedules for all laboratory and testing equipment. In a certified manufacturing plant, every production run undergoes rigorous quality assurance testing before shipping, including:
- Conductor Resistance Testing: Ensuring the electrical resistance per kilometer matches international standards (such as IEC 60228).
- Spark Testing and High-Voltage Checks: Passing insulated cores through high-voltage spark testers to instantly detect pinholes or insulation flaws.
- Tensile Strength and Elongation Tests: Verifying that the mechanical sheath can withstand the mechanical stress of pulling through conduits.
Root Cause Analysis and Corrective Action (CAPA)
In non-certified factories, if a batch of cables fails in the field, it is often swept under the rug. Under ISO 9001, every defect triggers a mandatory Corrective and Preventive Action (CAPA) protocol. The factory must investigate why the failure occurred, trace it back to the machine or process variable, and implement permanent engineering controls to ensure it never happens again. This relentless pursuit of continuous improvement means the cables you buy today are safer and more reliable than the ones produced last year.
Long-Term Cost Savings vs. Upfront Illusionary Savings
In project management, there is a dangerous temptation to view cable procurement as a commodity purchase where the lowest bidder wins. This is a false economy.
Consider the total lifecycle cost of an electrical installation:
- Initial Procurement: Uncertified cable might save you 5% to 10% on the initial bill of materials.
- The Hidden Risk: If a sub-standard cable fails behind a finished wall or inside an industrial cable tray two years later, replacing it requires tearing up drywall, shutting down factory operations, and paying for emergency electrical labor.
- The Catastrophic Cost: Worst of all, electrical fires caused by thermal overload can result in total asset loss, legal liability, and devastating safety hazards.
Choosing an ISO 9001 certified manufacturer guarantees peace of mind. You are paying for traceability, metallurgical consistency, and rigorous engineering compliance that protects your investment for decades.
Frequently Asked Questions (FAQs)
1. Does ISO 9001 certification mean the cable meets international standards like IEC or UL?
Not automatically. ISO 9001 is a Quality Management System certification that governs how a company manufactures its products. However, an ISO 9001 certified manufacturer is much more likely to consistently produce cables that comply with specific product standards like IEC, BS, or UL because their internal processes are tightly controlled and audited regularly.
2. How can I verify if a cable manufacturer is genuinely ISO 9001 certified?
Always ask the manufacturer for their current ISO 9001 certificate. A legitimate certificate will feature the accreditation body’s logo (such as UKAS, ANAB, or DAkkS) along with a traceable certificate number and an expiration date. You can verify the certificate directly on the issuing registrar’s online database.
3. Why is copper purity so critical in certified electrical cables?
Impure copper or sub-gauge sizing increases electrical resistance. Higher resistance generates excessive heat under normal electrical load, which accelerates insulation degradation, wastes electrical energy through transmission losses, and significantly raises the risk of electrical fires over time.
About the Author
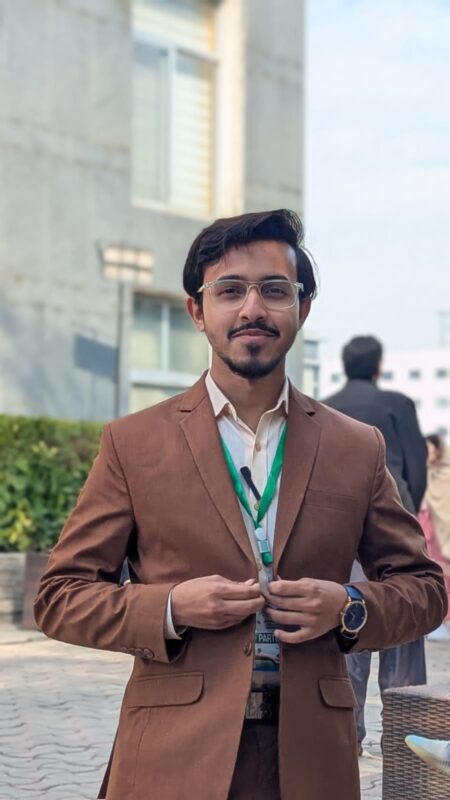
Ahmad Raza Ali is a Digital Marketing Manager and technical content strategist specializing in renewable energy infrastructure and industrial cable specifications. With a deep focus on search engine optimization and E-E-A-T principles, Ahmad bridges the gap between complex electrical engineering standards (IEC/BS) and practical consumer solar applications. He has been working with LifeCables.com; its sister company TaxAccountant.pk and MechaFuze an SEO Executive for long. He is a BBA cont. undergraduate as well with majors in marketing studying at SZABIST ISB.
